Reviewed for technical accuracy by Sunil Goyal, COO
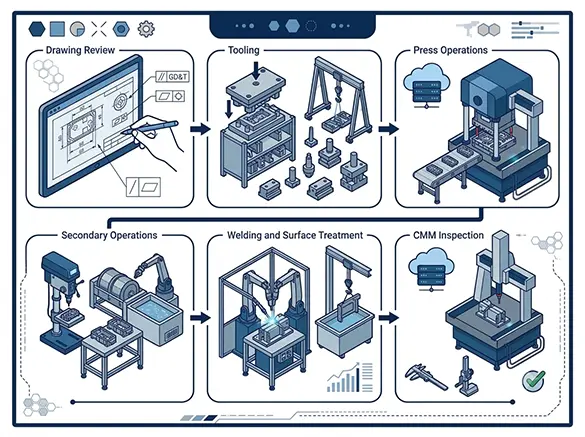
Presco-Mec Group is a pressed parts manufacturer in India, blanking, piercing and forming sheet metal components for automotive OEMs, Tier-1 suppliers and industrial equipment makers. With 38+ years of manufacturing experience, IATF 16949:2016 certified processes and two production units in Faridabad, Haryana, we take a pressed part from drawing review and tooling through press operations, secondary machining, welding, surface treatment and CMM inspection in one in-house process chain.
A pressed part is decided twice: once when the tool is designed, and again on every stroke of the press after that. The tool sets what the part can be; process control decides whether part ten thousand still matches the first-off sample. We plan for both, so your line receives a part that fits without rework, in the finish your drawing specifies. For the full component range and the applications we serve, see our pressed parts manufacturer and supplier in India page.
Share your component drawings, 3D CAD data, material specification and annual volumes with our engineering team for a feasibility review of your pressed parts programme.
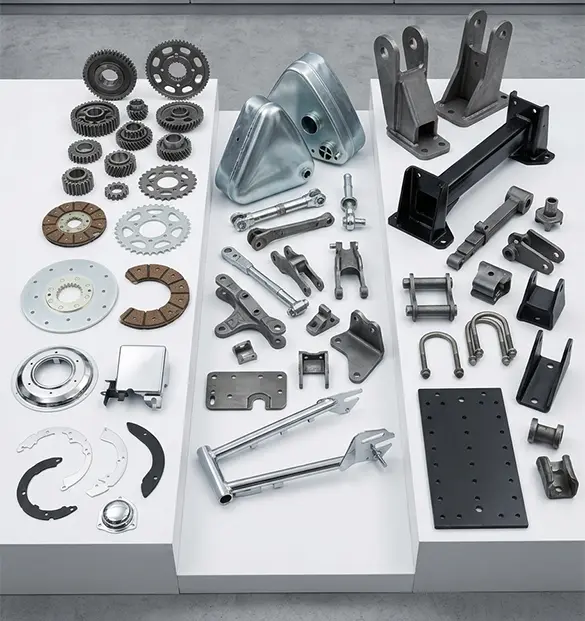
Submit Your RFQOur press shop, machine shop and weld shop produce pressed sheet metal components for structural, mounting and protective duty:
Each part is quoted against your drawing, material and volume, so the tooling route, press operations and finish are confirmed in our feasibility response rather than assumed.
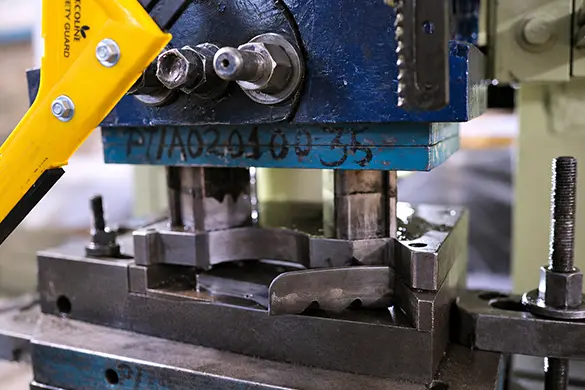
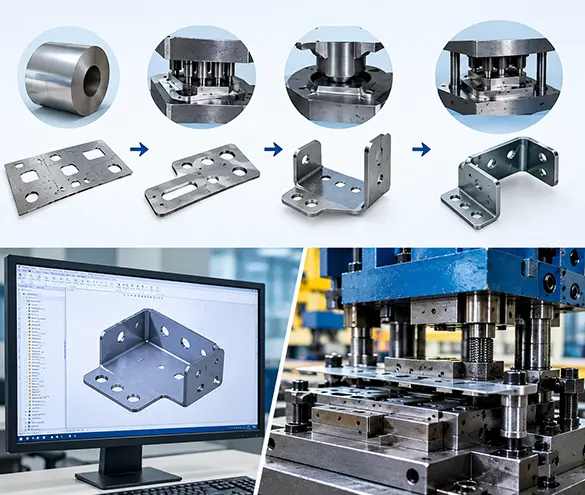
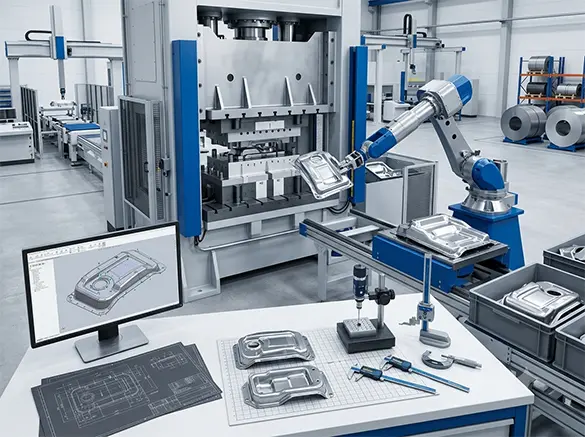
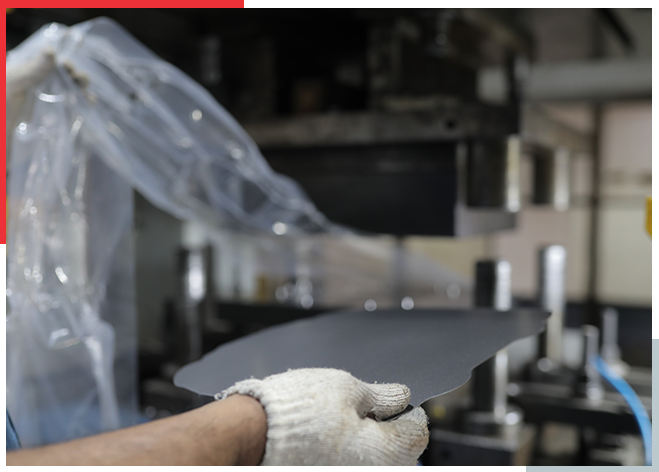
Most pressed parts pass through more than one operation. Blanking cuts the profile from coil or sheet, piercing adds holes and slots, forming and bending create the three-dimensional shape, and trimming finishes the edge. The sequence, the number of stages and the tool construction are chosen to suit the part geometry, the material grade and thickness, and the annual volume.
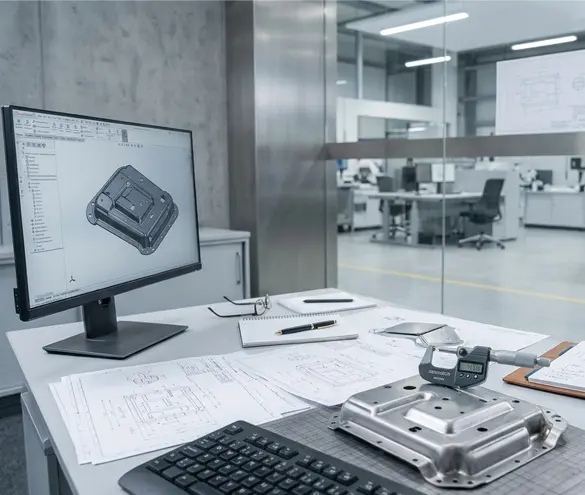
Tooling is designed in SolidWorks and CAD/CAM in coordination with your engineering team, and built through our in-house tool manufacturing facility or our associate tool rooms in India and Asia, depending on the programme. Because tool design and press operations sit with the same team, manufacturability feedback reaches your engineers before tooling is committed, not after first-off samples are rejected.
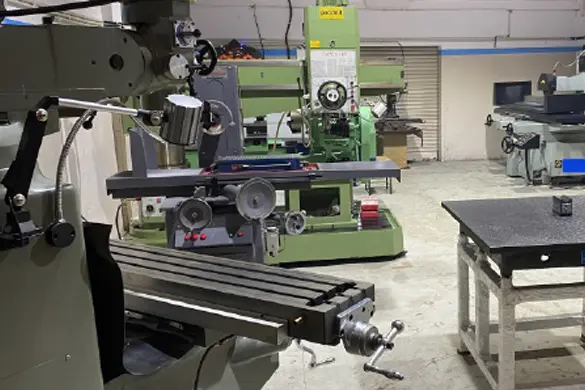
A part that leaves the press is rarely the part your line needs. Burrs, flatness and hole condition decide whether it fits at assembly without hand finishing. Our in-house machine shop carries out the secondary operations that turn a pressed part into a line-ready component: drilling, deburring and polishing, flattening and broaching.
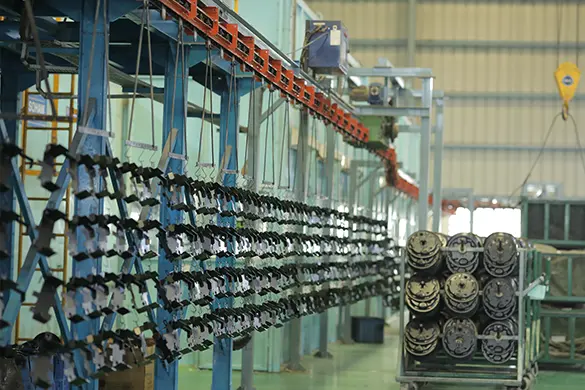
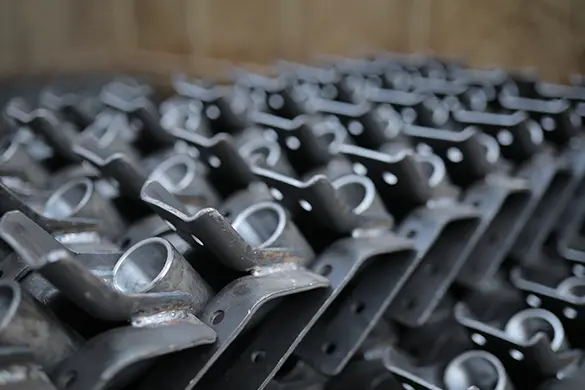
Where the drawing calls for a joined unit, our weld shop takes the pressed parts through MIG, robotic, spot or projection welding. Where it calls for corrosion protection, parts are processed on our PTCED line or conveyorised powder-coating line. Every stage runs in our own facilities, so one supplier is accountable for the part from coil to dispatch.
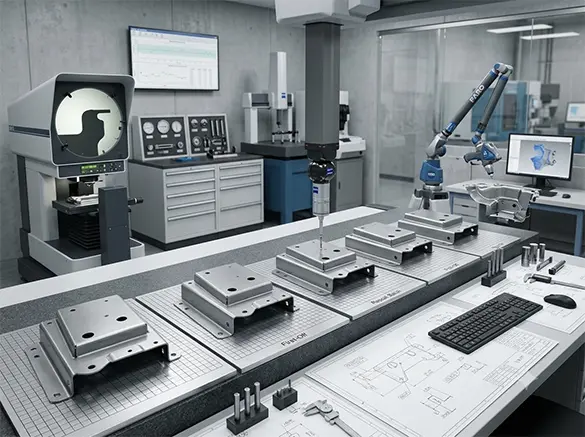
Pressed parts are bought in volume, and volume exposes drift. Tool wear, coil-to-coil variation in material and changes in press setting can move a hole position or a flange angle gradually over a production run, so a part that passed first-off inspection can still arrive out of tolerance months later. We manage this through process control and traceability from incoming material to final inspection, and by verifying critical dimensions in our standard room on CMM, Profile Projector and Faro Arm equipment before release. Tolerances are taken from your drawing, not assumed, so please flag critical-to-quality characteristics when you send your enquiry.
Our manufacturing operations are certified to internationally recognised automotive and quality standards.
IATF 16949:2016
ISO 9001:2015
ISO 14001:2015
ISO 45001:2018
Many pressed parts programmes start as a transfer rather than a new development: a current supplier is exiting, capacity is short, or a buyer wants to reduce vendor count. Send the current drawing, approved samples and details of the existing tooling, including who owns it. Our engineering team will review whether the existing tool can be run in our press shop or a new tool is required, and confirm what validation your programme needs before series supply begins.
The same press shop supplies pressed parts to two-wheeler, passenger vehicle, commercial vehicle, tractor and off-highway platforms, and to industrial applications. Procurement teams can consolidate several commodities with one audited vendor: brake parts, chassis and cabin parts, engine components, two-wheeler sheet metal parts, tractor sheet metal parts, off-highway sheet metal parts and automotive sub-assemblies.
To assess feasibility and prepare an accurate quotation, share as much of the following as is available:
Share your drawings and requirements through our Business Enquiry page to start a sourcing discussion.
Reviewed by Sunil Goyal, Chief Operating Officer
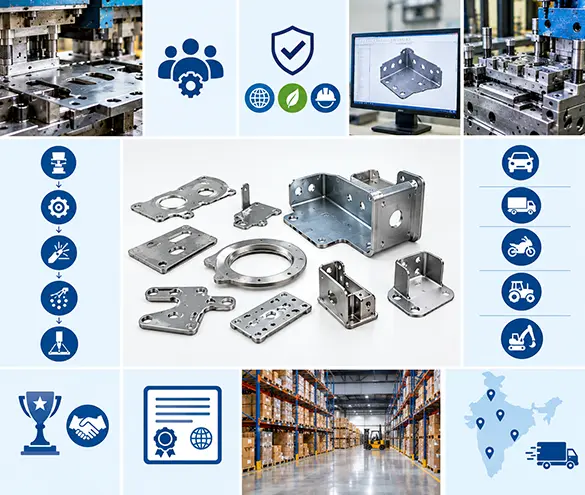
We manufacture pressed sheet metal components including structural brackets, mounting plates, gussets and support plates, cross-members and reinforcements, covers, guards, heat shields and baffle plates, panels, enclosures, mudguards and fenders, clamps and small formed parts, and custom parts pressed to customer drawings or approved samples.
Most parts combine blanking to cut the profile, piercing for holes and slots, forming and bending for the three-dimensional shape, and trimming to finish the edge. The sequence and the number of stages are chosen to suit the part geometry, material grade, thickness and annual volume.
Tooling is designed in SolidWorks and CAD/CAM in coordination with your engineering team. Depending on the programme, it is built in our in-house tool manufacturing facility or through our associate tool rooms in India and Asia, and the route is confirmed in our feasibility response.
Our in-house machine shop carries out drilling, deburring and polishing, flattening and broaching, so pressed parts arrive ready to fit. Parts can also be welded into sub-assemblies and finished on our PTCED or conveyorised powder-coating lines.
Tool wear, material variation and press settings can shift dimensions gradually over a run, so we maintain process control and traceability from incoming material to final inspection, and verify critical dimensions on CMM, Profile Projector and Faro Arm equipment before release.
Often, yes. Share the current drawing, approved samples and details of the existing tooling, including who owns it. Our engineering team will confirm whether the existing tool can be used or a new tool is required, and what validation is needed before series supply.
Yes. Share your annual volume, batch sizes and ramp-up plan with your enquiry, and our engineering team will confirm a tooling and production approach suited to that volume.
Yes. The same press shop supplies brake, chassis and cabin, engine, two-wheeler, tractor and off-highway parts, so procurement teams can consolidate several commodities with one IATF 16949:2016 certified vendor.
Send drawings or 3D models, material grade and thickness, critical dimensions, secondary-operation and finish requirements, annual volumes and target timelines through our Business Enquiry page or to info@prescomecgroup.com. Our engineering team will revert with a feasibility response.
Last updated:
If you are sourcing pressed sheet metal parts in India, share your drawings, material specification and annual volumes with our engineering team through our Business Enquiry page or at info@prescomecgroup.com. We will revert with a feasibility response.
Contact Us