Automotive Sub-Assembly Manufacturer in India

Reviewed for technical accuracy by Sunil Goyal, COO
Welded steel sub-assembly for an automotive application

Looking for an Automotive Sub-Assembly Manufacturer?

Share your component drawings, 3D CAD data, and manufacturing requirements with our engineering team for a feasibility review and a customized automotive sub-assembly solution.

Submit Your RFQ

Sub-Assemblies We Manufacture for Automotive OEMs

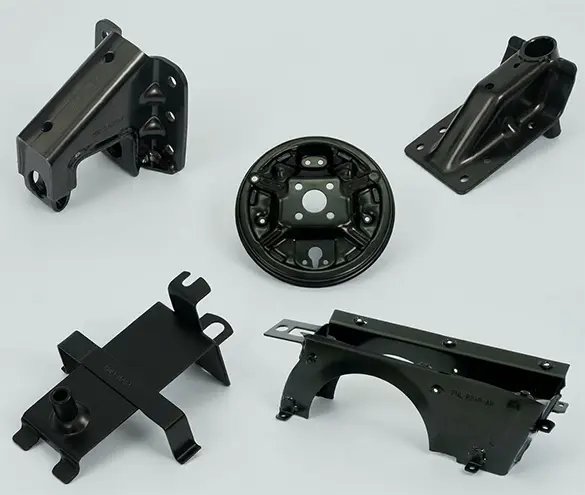
Our press shop and weld shop produce welded sub-assemblies across several vehicle platforms:

Welded steel bracket sub-assemblies on a workbench
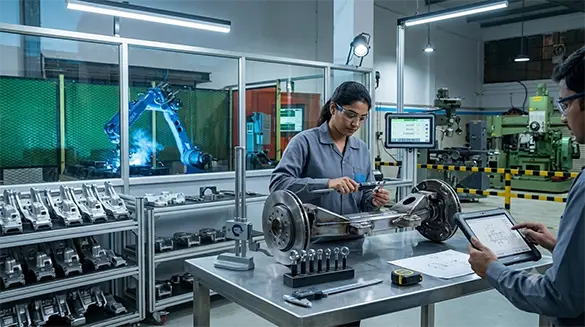
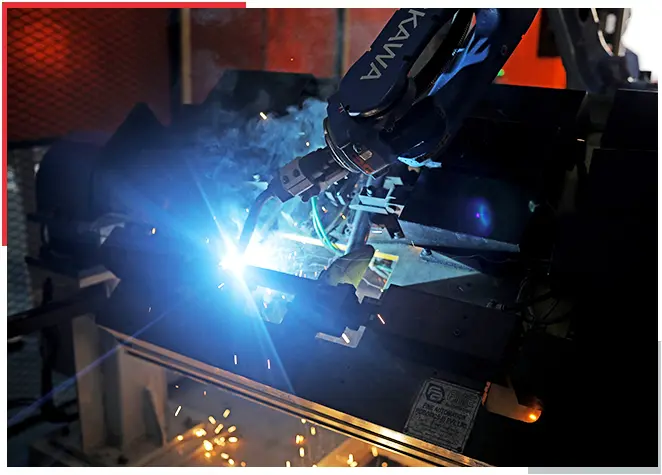
Robotic welding and inspection of a sheet metal sub-assembly

Why OEMs and Tier-1s Choose Presco-Mec Group for Sub-Assemblies

  • Fewer supplier hand-offs: stamping, welding, finishing and inspection under one roof
  • 38+ years of manufacturing experience and 200+ team members
  • IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018 certified units, detailed on our Quality Profile page
  • In-house tooling design and development
  • 25+ industry awards and 10+ OEM and Tier-1 relationships, see our featured customers
  • D&B D-U-N-S registered (65-006-5357) for vendor onboarding
  • Warehouses in Pithampur, Jamshedpur, Pune and Chennai for delivery close to your plant, see all manufacturing locations

Controlling Tolerance Stack-Up at Every Joint

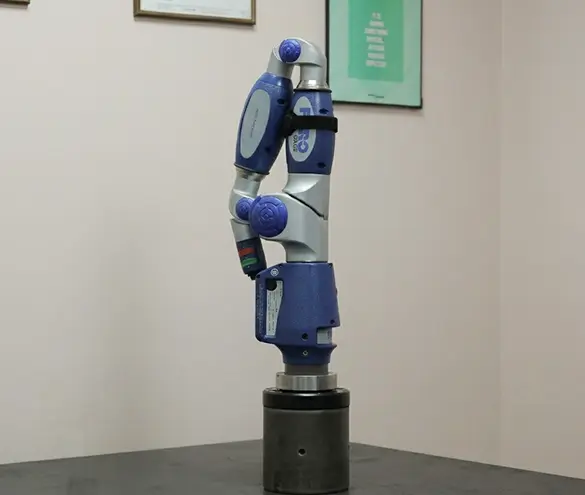
In a multi-piece welded assembly, small dimensional variances at any single part or joint can compound. We address this at each stage. Tooling is designed in SolidWorks and CAD/CAM in coordination with the customer, so the parts are built for repeatable production before a single piece is stamped. Components are joined using MIG, robotic, spot and projection welding, with purpose-built SPMs (Special Purpose Machines) deployed where they improve consistency at volume. Finished units are then measured in our standard room on CMM, Profile Projector and Faro Arm equipment, so stack-up is caught before an assembly reaches your line.

Measuring arm checking a welded automotive component
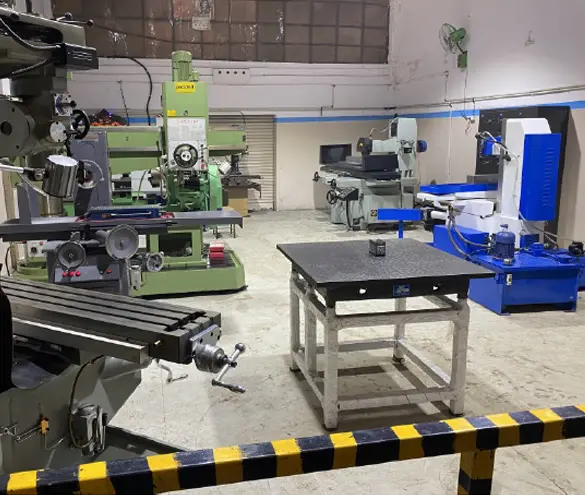
Dimensional and surface-finish check on a welded sheet metal component

A Quality-Focused Sub-Assembly Supplier

Our IATF 16949:2016 quality management system governs process control from incoming raw material through to final assembly, and it is the same system our brake, chassis and cabin, and engine parts customers already rely on. For sub-assemblies, that discipline translates into:

  • Consistent weld quality across production batches
  • Dimensional accuracy verified before dispatch
  • Finish consistency through controlled coating processes
  • One point of accountability for fitment, finish and delivery

From Component to Sub-Assembly: Our Integrated Process

  • Tool design and development: Engineer tooling with the customer for repeatable, large-scale production.
  • Stamping: Form components in the press shop to hold dimensional tolerances.
  • Welding and joining: Join parts into sub-assemblies using MIG, robotic, spot or projection welding.
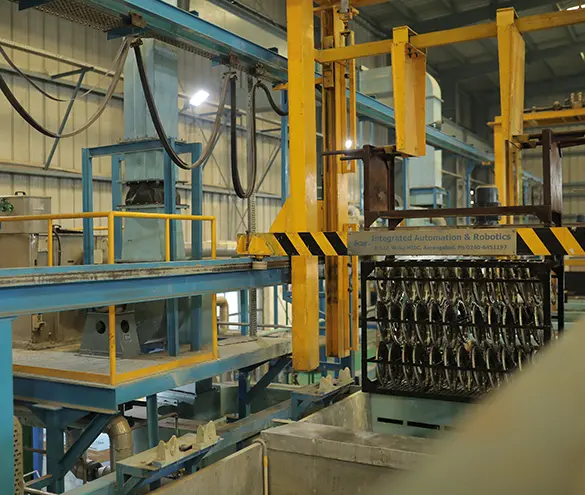
  • Surface finishing: Apply PTCED or powder coating as the application specifies.
  • Inspection and release: Verify the assembly against drawing tolerance before dispatch.
Welding fixture holding sheet metal parts during joining
Structural steel assemblies for vehicle platforms

Programmes and Platforms We Support

Sourcing teams rarely buy for a single platform. Because every sub-assembly follows the same certified sequence, OEMs can consolidate several part families, from two-wheeler to tractor and off-highway, with one supplier instead of re-qualifying a vendor for each programme. Finishing is carried out on our PTCED and conveyorised powder-coating lines, and you can review our manufacturing infrastructure before shortlisting.

FAQ

We join stamped and formed sheet metal components such as brackets, mounts, frame members and structural panels into welded sub-assemblies that arrive ready to fit on your line.

Stamping, welding, surface finishing and inspection happen within our two Faridabad units, so your team audits one quality system and deals with one point of accountability instead of coordinating separate stamping, welding and coating vendors.

Tolerance stack-up is the accumulation of small dimensional variations across every part and joint in an assembly. In multi-piece welded units it can affect final fitment, which is why we verify assemblies on CMM, Profile Projector and Faro Arm equipment before dispatch.

Assemblies can be finished on our PTCED (cathode electro deposition) line or our conveyorised powder-coating line, depending on the corrosion resistance and finish your application specifies.

Tooling is designed in SolidWorks and CAD/CAM in coordination with the customer. Purpose-built SPMs (Special Purpose Machines), developed with established equipment partners, are deployed where they improve weld consistency at production volumes.

Yes. We build structural assemblies for tractors and off-highway applications, which typically face higher load and vibration duty cycles than passenger vehicle components.

Yes. Because every assembly follows the same tooling, stamping, joining, finishing and inspection sequence, OEMs can consolidate several part families without re-qualifying a new vendor for each platform.

Yes. The IATF 16949:2016 quality management system governs process control from incoming raw material to final assembly across all our product lines, including brake, chassis and cabin, and engine parts.

Our certifications are listed on the Quality Profile page, and our D&B D-U-N-S number (65-006-5357) is available for vendor onboarding. Manufacturing locations are listed on our Manufacturing page.

Send your part drawings or 3D models, annual volumes and any finish specification through our Business Enquiry page or write to info@prescomecgroup.com. Our engineering team will confirm feasibility.

Last updated:

Partner with a Trusted Automotive Sub-Assembly Manufacturer in India

If you are evaluating an automotive sub-assembly manufacturer in India for an upcoming sourcing programme, share your drawings, annual volumes and finish specification with our engineering team. We will revert with a feasibility response.

Contact Us